
Can a contrast sensor be used in the printing industry?
As a supplier of contrast sensors, I am often asked about the applicability of these sensors in various industries, especially the printing industry. In this blog post, I will explore the potential uses of contrast sensors in the printing industry and explain why they can be a valuable addition to printing processes.
Understanding Contrast Sensors
Before delving into their use in the printing industry, let's first understand what contrast sensors are. A Contrast Sensor is a type of optoelectronic sensor that detects the difference in reflectivity between two adjacent areas. It emits a light beam onto a surface and measures the amount of light reflected back. By comparing the reflectivity of different areas, the sensor can distinguish between objects or markings with different colors, shades, or patterns.
Contrast sensors are highly versatile and can be used in a wide range of applications, including packaging, food and beverage, automotive, and, of course, the printing industry. They offer several advantages, such as high precision, fast response times, and the ability to work in various environmental conditions.
Applications of Contrast Sensors in the Printing Industry
- Print Registration
One of the most critical aspects of the printing process is print registration, which refers to the accurate alignment of different colors or printing elements on a substrate. Misregistration can result in blurred or overlapping prints, leading to poor quality and wasted materials. Contrast sensors can play a crucial role in ensuring print registration by detecting registration marks on the substrate.
Registration marks are small, distinct markings placed on the printed material at specific locations. These marks can be of a different color or pattern compared to the surrounding area. Contrast sensors can detect these marks with high precision and provide feedback to the printing press control system. The control system can then adjust the position of the printing plates or the substrate to ensure accurate alignment, resulting in sharp and clear prints.
- Color Quality Control
In the printing industry, maintaining consistent color quality is essential to meet customer expectations and brand standards. Contrast sensors can be used in color quality control processes to monitor and verify the color accuracy of printed materials.
By measuring the contrast between different color areas on the print, contrast sensors can detect any variations in color intensity or hue. This information can be used to adjust the printing parameters, such as ink flow or color mixing, to ensure that the printed colors match the desired specifications. Additionally, contrast sensors can be used to detect color defects, such as color streaks or uneven color distribution, allowing for immediate corrective action to be taken.
- Print Inspection
Print inspection is another important application of contrast sensors in the printing industry. After the printing process, it is necessary to inspect the printed materials for any defects, such as missing or smudged prints, ink splatters, or damaged areas. Contrast sensors can be used to perform automated print inspection by detecting the contrast differences between the printed areas and the background.
The sensors can scan the printed material at high speeds and identify any areas where the contrast deviates from the expected values. This allows for the detection of defects in real-time, enabling prompt rejection of defective prints and reducing the risk of faulty products reaching the market.
- Web Guiding
In web-fed printing presses, the substrate is fed continuously in the form of a web. Maintaining the proper alignment of the web is crucial to ensure smooth and efficient printing operations. Contrast sensors can be used in web guiding systems to detect the edges of the web and provide feedback to the guiding mechanism.
By measuring the contrast between the web and the surrounding area, the sensors can accurately determine the position of the web edges. The guiding system can then adjust the position of the web to keep it centered and prevent it from drifting or wrinkling during the printing process. This helps to improve the overall printing quality and reduce the risk of web breaks or jams.
- Counter Sensor Integration
In some printing applications, it may be necessary to count the number of printed sheets or labels. Counter Sensor can be integrated with contrast sensors to provide accurate counting functionality.
Contrast sensors can detect the presence of printed materials, and the counter sensors can increment the count each time a new item is detected. This combination of sensors can be used in printing presses, labelers, or other equipment to keep track of the production volume and ensure accurate inventory management.
Advantages of Using Contrast Sensors in the Printing Industry
-
High Precision and Accuracy
Contrast sensors offer high precision and accuracy in detecting small differences in reflectivity, making them suitable for applications that require precise measurements, such as print registration and color quality control. Their ability to detect even subtle variations in contrast allows for accurate detection of registration marks, color defects, and other critical features in the printing process. -
Fast Response Times
In the fast-paced printing industry, speed is of the essence. Contrast sensors have fast response times, which means they can detect changes in contrast quickly and provide immediate feedback. This allows for real-time adjustments to the printing process, minimizing downtime and improving productivity.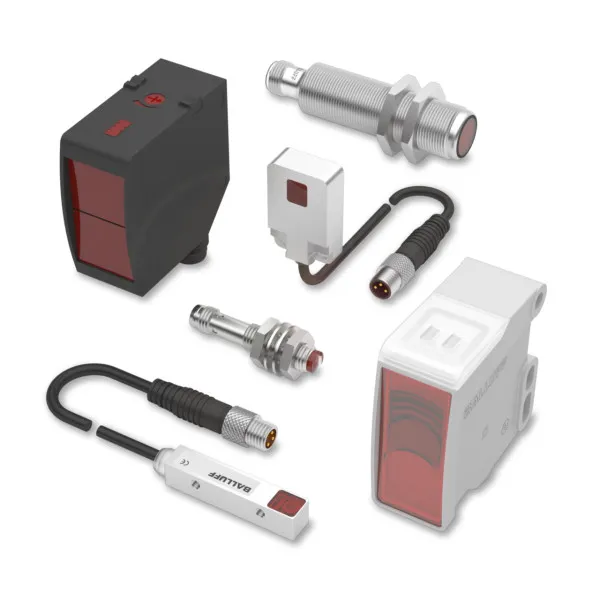
-
Versatility
Contrast sensors are highly versatile and can be used in a variety of printing applications, from small-scale label printing to large-format commercial printing. They can work with different types of substrates, including paper, cardboard, plastic, and metal, and can detect a wide range of colors and patterns. -
Cost-Effectiveness
By improving print quality, reducing waste, and increasing productivity, contrast sensors can provide significant cost savings in the long run. The initial investment in contrast sensors is relatively low compared to the potential benefits they offer, such as reduced rework, lower material costs, and improved customer satisfaction.
Challenges and Considerations
While contrast sensors offer many benefits in the printing industry, there are also some challenges and considerations that need to be addressed.
-
Surface Reflectivity
The performance of contrast sensors can be affected by the surface reflectivity of the substrate. Highly reflective or glossy surfaces can cause reflections and glare, which may interfere with the sensor's ability to accurately detect contrast. In such cases, special techniques or sensor configurations may be required to minimize the effects of surface reflectivity. -
Environmental Conditions
The printing environment can be harsh, with factors such as dust, heat, humidity, and vibration. These environmental conditions can affect the performance and reliability of contrast sensors. It is important to choose sensors that are designed to withstand these conditions and to provide proper protection and maintenance to ensure their long-term operation. -
Calibration and Setup
Proper calibration and setup of contrast sensors are essential to ensure accurate and reliable operation. The sensors need to be calibrated to the specific printing materials and conditions to achieve optimal performance. This may require some technical expertise and knowledge of the sensor's operating principles.
Conclusion
In conclusion, contrast sensors can be a valuable tool in the printing industry, offering a range of applications from print registration and color quality control to print inspection and web guiding. Their high precision, fast response times, versatility, and cost-effectiveness make them an attractive option for printing companies looking to improve their printing quality, productivity, and efficiency.
However, it is important to carefully consider the specific requirements of the printing process and the environmental conditions when selecting and using contrast sensors. By addressing the challenges and considerations mentioned above and working with a reliable sensor supplier, printing companies can successfully integrate contrast sensors into their operations and reap the benefits they offer.
If you are interested in learning more about how contrast sensors can benefit your printing processes or if you are looking for a reliable contrast sensor supplier, please feel free to contact us. We have a team of experts who can provide you with detailed information and assistance in selecting the right sensors for your needs. Let's work together to enhance your printing quality and efficiency.
References
- "Optoelectronic Sensors in the Printing Industry" - Industry White Paper
- "Printing Technology: Principles and Practices" - Textbook on Printing Processes
- Manufacturer's Documentation on Contrast Sensors and Their Applications